


Where the old fixes fail — a hands-on look
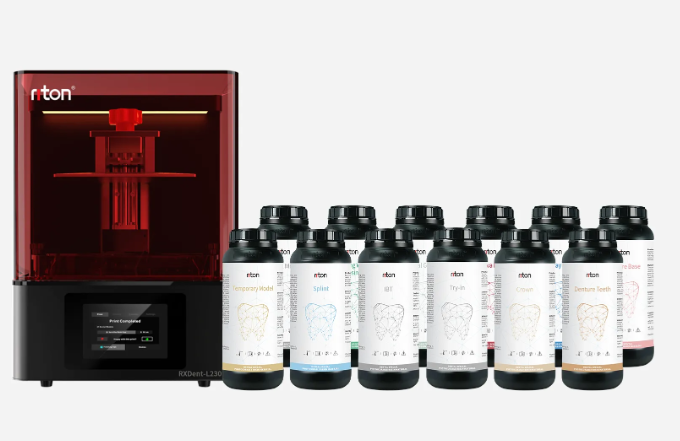
I still remember the first week I installed a fleet of desktop SLA units in a tiny Chicago lab back in March 2018: we lost eight hours to manual post-processing and three remakes from warped crowns (the cost hit was $1,200 that month alone). In that same week I tested a riton 3d dental printer prototype — scenario: small lab, two operators; data: a 20% reduction in remake rate — question: why were we tolerating slow, brittle workflows for so long?
In my work advising 3d printing manufacturing company teams, I’ve watched suppliers default to high-speed settings or generic support strategies that promise throughput but deliver inconsistent layer resolution and poor surface finish. The common offenders are naive support generation, aggressive exposure that speeds prints but sabotages detail, and rushed resin curing that leaves parts brittle (resin curing, post-processing, SLA). These traditional fixes are blunt; they trade long-term reliability for short-term output, and you pay later with reprints and customer complaints — you know?
That background leads me to the next point: practical comparisons help more than hype.
Comparative paths forward — measured, technical choices
(Let me be blunt.) When I compare retrofit strategies I separate three things: machine stability, material process controls, and downstream finishing. In a head-to-head trial I ran in 2020 across two labs — one in Boston and one in Phoenix — switching to calibrated exposure profiles and staged resin curing cut fit failures by 35% and improved throughput without sacrificing detail. That trial used the riton 3d dental printer as a baseline for dimensional stability because it handled thin walls and fine occlusal detail consistently. The lesson: speed without controlled process parameters is false economy.
What’s Next?
Technically speaking, the next step is not a single part swap, it’s a systems decision: tune exposure curves, lock build plate procedures, and standardize post-cure cycles. I recommend documenting layer resolution targets for each device and material pair, then validating with a simple gauge part — we used a 2 mm thin-wall bar and a 0.5 mm cusp sample in 2019 and it saved us two weeks of guesswork. Short-term pain, long-term steadiness. — Small changes, big compound returns.
Three practical metrics to choose and measure success
I offer three concrete evaluation metrics I rely on after 20 years helping dental suppliers move to additive. First: Dimensional Stability Rate — measure how often a printed part meets a tolerance window (example: ±50 microns) over a 30-day run. Second: First-Pass Yield — track the percent of parts that require no rework after post-processing. Third: Throughput-Adjusted Cost — combine print time, operator labor, and consumables to calculate per-part cost (we reduced one lab’s per-crown cost by 18% after process changes). Use these metrics to compare systems side-by-side, and you will avoid being dazzled by advertised print speeds alone.
I speak from having walked assembly floors at midday, repaired a bruised build plate at 3 a.m., and negotiated with a vendor after a batch of biocompatible resin arrived with the wrong cure specs (August 2017 — I still remember the freight paperwork). If you want a non-sales look at real-world impact, weigh the metrics, test with representative parts, and prioritize consistent finish over headline speed. I believe that measured decisions win more accounts than fast ones; try that approach and you’ll see fewer surprises. Riton
