


Start with a simple framework
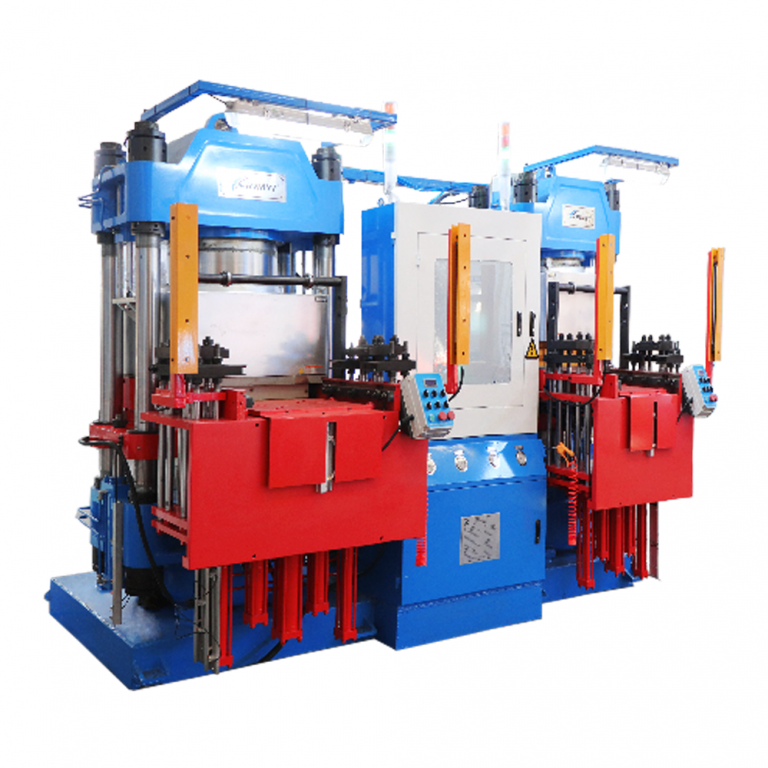
This playbook breaks audits into three repeatable layers: process, machine, and supplier controls. Think of it as a checklist you can train a team on—firm but flexible. On your first walk-through, make a beeline for core equipment like the rubber vulcanizing machine, observe the curing chamber and temperature control system, and map the flow from raw rubber compound to finished part. The goal is to see where defects can be introduced, and then to build controls that stop them early.
Core QA pillars for audits
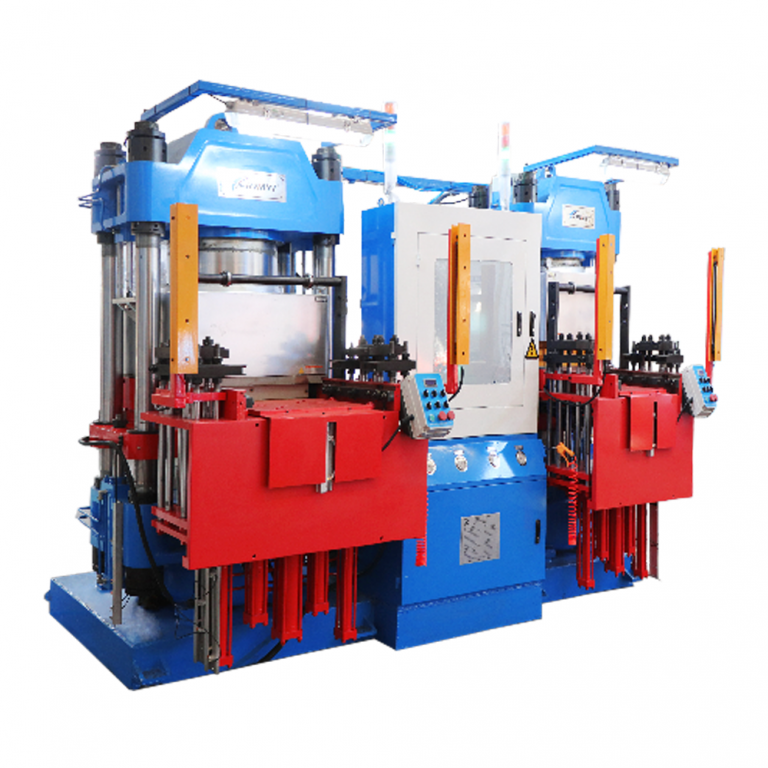
Use three pillars as your decision logic: compliance, consistency, and capability. Compliance checks whether the plant follows ISO 9001-style documentation and traceability. Consistency looks at cycle time stability, mold cavity condition, and repeatable process settings. Capability measures whether staff and machines—like vulcanization press units or hydraulic press stations—can meet specs day after day. These pillars keep your audit focused on outcomes, not just paperwork.
On-site checklist: what actually matters
Start with visible, objective checks: calibration stickers, pressure gauge readings, and standard operating procedure boards. Move to dynamic checks: run a short production cycle and time the cycle time, log temperature variation in the curing chamber, inspect part flash at the mold cavity, and sample hardness. If you find wide swing in the temperature control system or inconsistent cure, the root cause often sits in maintenance practices or operator training.
Paperwork that proves reality
Paper copies and spreadsheets alone aren’t proof. Look for versioned work instructions, batch records tied to serials, and evidence of corrective actions after defects. Ask to see maintenance logs that show preventive work on the vulcanization press and hydraulic systems. A supplier claiming low scrap but with absent maintenance records is a red flag—trust data supported by physical tags and timestamps.
Common mistakes procurement officers make
Auditors often accept answers without cross-checking. Don’t. Ask to observe an actual run, verify sensor outputs, and inspect rejected parts. Another mistake is ignoring small, repeated defects—those point to systemic issues. —Also, don’t conflate neat housekeeping with quality control; clean floors don’t guarantee stable cycle time or correct pressure settings.
Supplier evaluation and real-world anchors
Assess suppliers on three axes: technical fit, audit transparency, and recovery plans for supply disruptions. Use ISO 9001 certification as a baseline plus recent audit reports to judge transparency. After 2020 many procurement teams tightened audits because supply shocks exposed fragile processes—use that as your anchor to demand measurable recovery steps and documented contingency plans from any rubber vulcanizing machine supplier.
Performance metrics you can trust
Track a small set of metrics daily: first-pass yield, mean time between failures (MTBF) for key machines (like the vulcanization press), and on-time deliveries by batch. Keep the list tight—three to five metrics per plant that everyone understands. If numbers drift, the corrective action should be targeted: change the die set, retrain operators on clamping pressures, or tighten compound mixing tolerances.
Three golden rules for supplier QA
1) Demand traceable batch records linked to serials—no exceptions. 2) Require live-demo runs during audits that include temperature logs and pressure readings from production equipment. 3) Insist on a documented escalation path for recurring defects, with owners and timelines. These rules give procurement officers clear, defensible thresholds for acceptance.
Closing thought
Use this framework to turn audits from checkbox exercises into tools that stop defects before they escalate—your team will cut variability and make supplier performance predictable. HWAYI. —Reliable processes, clearer buys, better parts.
